
Solving High Risk Mining MRO Challenges
John Crane retrofit helps copper mine save around 288,000 liters of sealing water per day on critical tailings pump
John Crane took its sealing knowledge from general industry and oil and gas and applied this expertise to the mining industry.
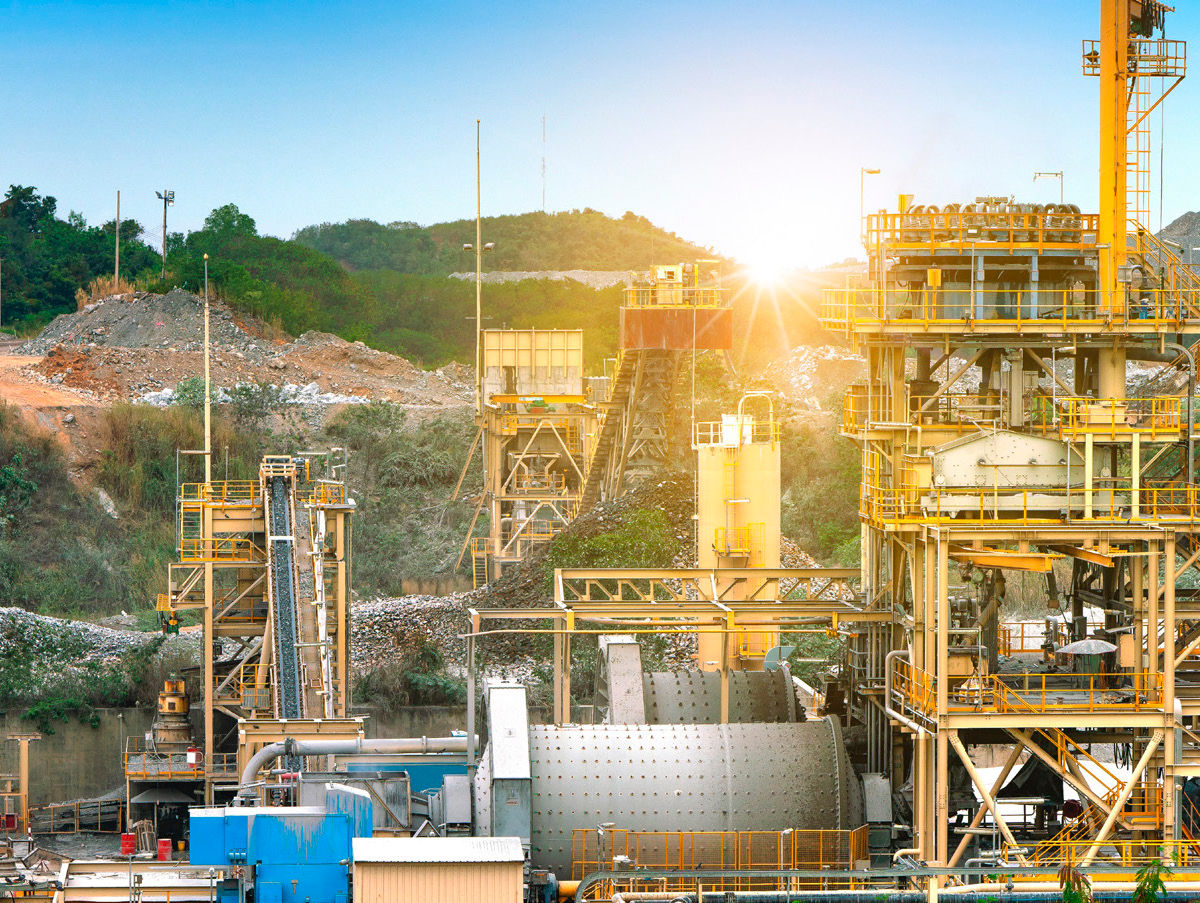
John Crane, a business unit of Smiths Group plc, has retrofitted a mechanical seal on a large underflow thickener slurry pump at a major copper mining operation, cutting the clean water needed for sealing by around 288,000 liters per day and supporting a move away from frequent, high-risk maintenance interventions on a production-critical asset. With a shaft diameter of approximately 270 mm, the installation represents the largest slurry seal sold by John Crane to date.
“Underflow thickener pumps are among the most critical assets in a mine’s tailings circuit, so customers are understandably cautious about change,” said Warren Smith, global mining market director, John Crane. “This project is a practical example of how improved sealing can reduce maintenance exposure and cut the clean water required for sealing, while supporting more predictable planned maintenance.”
Mining Pump Maintenance
Smith has been involved in the mining industry for 26-plus years in a variety of positions including product development, sales, and even working on pumps in the field. He has been involved in fluid dynamics and sealing in mining as well as general industrial applications.
Regarding slurry pump maintenance, Smith said the stuffing box is the chamber through which the rotating shaft passes and which the packing is installed. The packing is designed to control leakage around the shaft, while clean gland water helps cool and lubricate the packing and limit the entry of abrasive slurry. Correct selection, installation and adjustment of the packing are important to keep pumps running longer and more efficiently.
Underflow thickener pumps are a key link in tailings handling, moving high-density slurry from the thickener into the tailings transport system. In this application, the Warman 550 pump operates at approximately 65 percent solids, where reliability is essential and any unplanned interruption can have an immediate impact on production.